Explore heavy-duty, boltless, and custom-engineered racking modules for commercial and industrial deployments.
Analyzing supply chain shift, structural steel advantages, and cost-efficiency benchmarks in modern logistics infrastructure.
The global logistics and warehousing market is undergoing a seismic transformation driven by the exponential growth of e-commerce, automated fulfillment infrastructure, and rapid industrialization across emerging markets. Procurement executives, supply chain directors, and warehouse planning engineers face an urgent imperative: optimizing floor cubic efficiency while ensuring maximum structural integrity, compliance safety, and cost scalability. Within this macro landscape, sourcing enterprise industrial racking systems directly from top-tier Chinese manufacturers has transitioned from a purely cost-saving tactic to a core strategic advantage.
China accounts for a substantial percentage of the world's structural steel processing capacity and cold-rolled coil production. Key industrial hubs, particularly in advanced manufacturing belts like Shenzhen and Guangdong province, offer an unmatched ecosystem of raw material availability, automated precision machining, skilled metallurgical engineering, and robust deep-water export logistics. When evaluated against Search Quality Rater Guidelines (E-E-A-T), top Chinese sourcing partners demonstrate verifiable technical authority and localized adaptability to international building standards.
Strategic Sourcing Insight: Enterprise procurement teams leveraging direct factory partnerships in China achieve an average of 35% to 48% overall TCO (Total Cost of Ownership) reduction compared to localized regional distributors, without compromising structural certification standards such as ANSI/RMI MH16.1, FEM 10.2.02, or ISO 9001 quality management.
Modern global sourcing strategies demand more than just transactional purchasing; they require deep collaboration with OEMs (Original Equipment Manufacturers) capable of engineering bespoke load-bearing systems. Whether installing heavy-duty selective pallet racks designed for 3,000 kg dynamic loads per level, or deploying modular boltless shelving units for micro-fulfillment centers, industrial buyers must evaluate potential suppliers based on raw material traceability, structural FEA (Finite Element Analysis) simulation tools, and automated surface treatment pipelines.
Technical evaluation of warehouse racking topologies, load parameters, and industry-specific deployment scenarios.
Selecting the optimal industrial racking architecture requires matching operational workflows (FIFO vs. LIFO, manual picking vs. AGV automation) with exact structural engineering specifications. Below is an authoritative technical classification of enterprise storage systems available from primary Chinese suppliers:
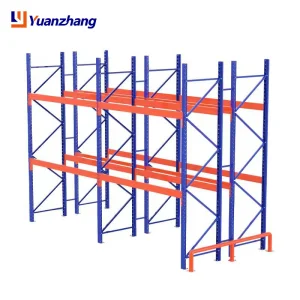
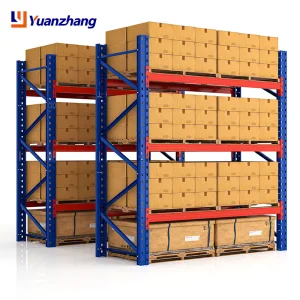
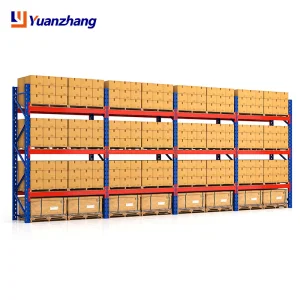
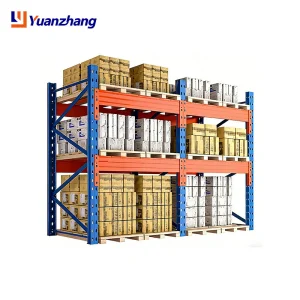
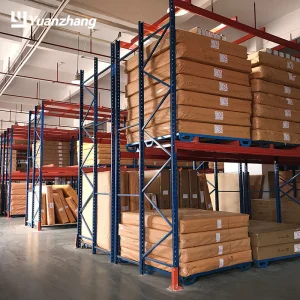
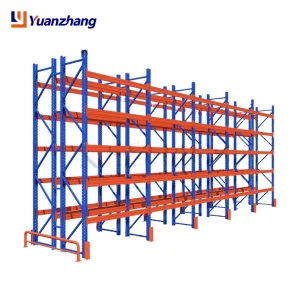
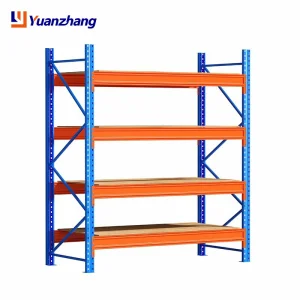
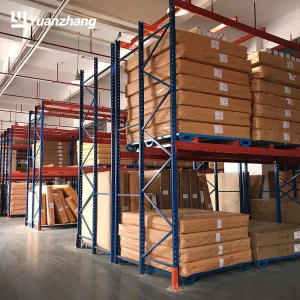
The standard choice for maximum versatility. Offers 100% immediate access to every pallet position. Engineered with adjustable beam profiles, teardrop or diamond upright punching, supporting unit capacities up to 3,000 kg per level.
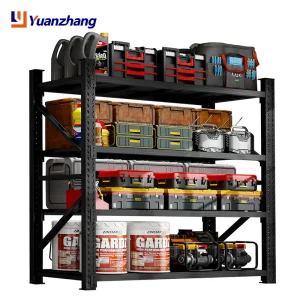
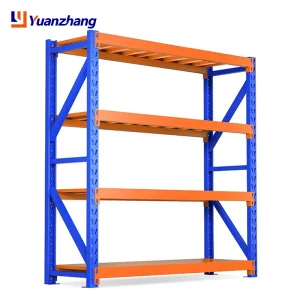
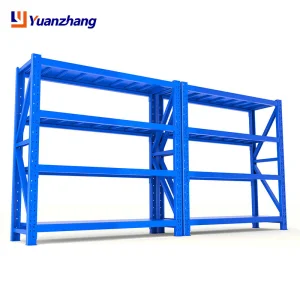
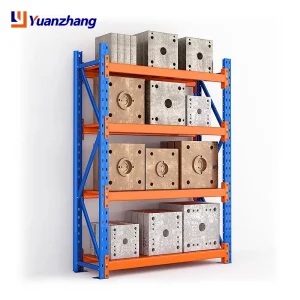
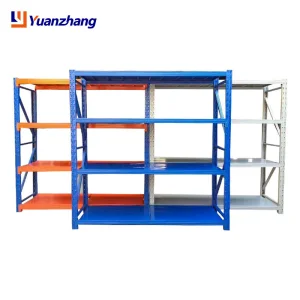
Ideal for hand-loaded boxed cargo, retail inventory, and industrial maintenance tools. Configured with 200 kg to 800 kg load capacity per layer, utilizing cold-rolled steel decking, wire mesh, or chipboard panels with boltless teardrop clips.
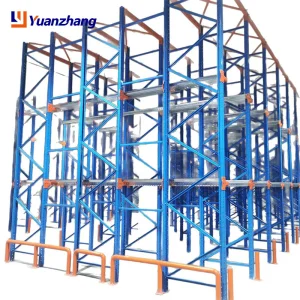
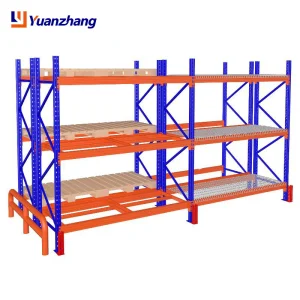
High-density solutions that maximize volume by eliminating aisle space. Perfect for high-volume uniform SKU stock, cold storage operations, and raw material buffer warehouses requiring high floor-space utilization.
Flexible, portable stacking units designed for seasonal inventory surges or irregular heavy components. Stackable up to 4–5 tiers high when loaded, collapsing down flat when empty to optimize return logistics.
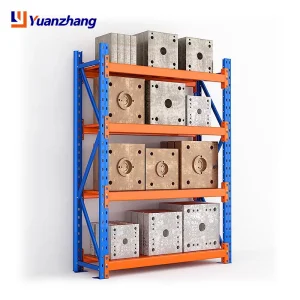
Modern industrial projects frequently integrate specialized applications including Cold Storage (with specialized low-temperature anti-brittle steel alloys), Automated Storage and Retrieval Systems (AS/RS) compatible racking grids, and heavy equipment parts storage for automotive assembly lines.
Demonstrating industry-leading E-E-A-T through global scale, R&D capabilities, and quality control infrastructure.
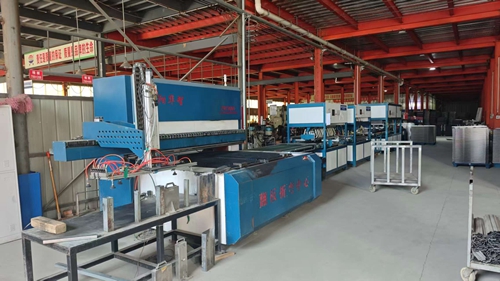
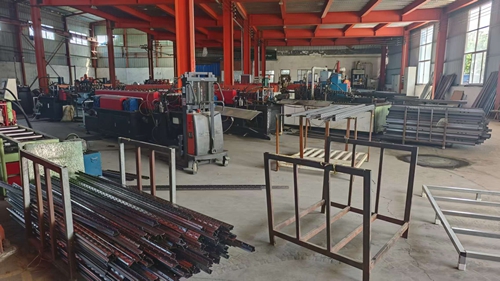
Established in 2015, Shenzhen Yuanzhang Trading Co., Ltd. has established itself as a premier enterprise manufacturer and exporter specializing in heavy-duty warehouse racking and customized industrial storage systems. Operating out of a state-of-the-art 35,000 m² production facility, the company combines over 12 years of deep industry expertise with 8 years of dedicated international trade experience serving global logistics and commercial infrastructure projects.
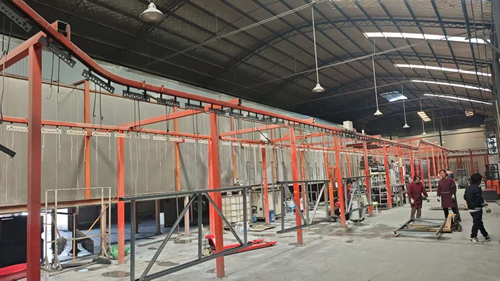
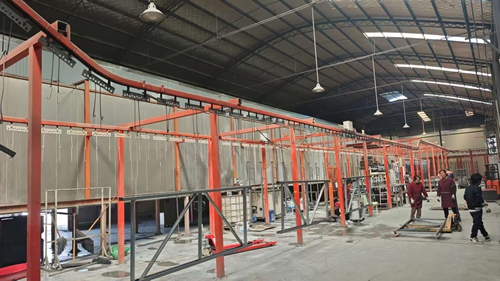
Driven by technical innovation, operations are anchored by a dedicated research and development hub powered by 25 expert R&D engineers. Demonstrating market leadership and responsiveness to evolving supply chain demands, the team launched over 150 new storage solutions last year alone. Full-spectrum OEM/ODM capabilities allow comprehensive customization, including non-standard beam lengths, specialized upright profiles, weight capacity adjustments, electrostatic powder coating formulations, and fully integrated modular structural frames.
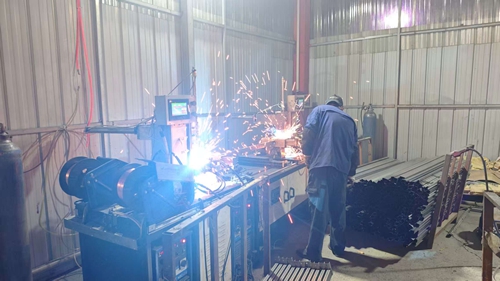
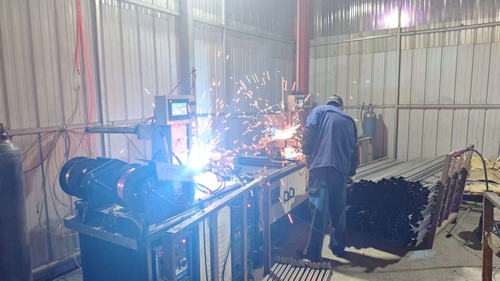
Quality assurance forms the core foundation of product reliability. Shenzhen Yuanzhang Trading Co., Ltd. enforces a multi-stage quality control protocol led by a team of 45 QA/QC inspectors. Testing methodologies include raw material stress analysis, automated ultrasonic weld checking, zinc plating thickness verification, and heavy load-bearing fatigue assessments.
With annual export revenue reaching $28 million USD and a resilient supply network of over 800 strategic raw material and component partners, the factory maintains reliable lead times across international markets. Primary export destinations span North America, Western Europe, Southeast Asia, and the Middle East, serving major 3PL logistics networks, industrial distributors, automated fulfillment centers, and commercial retail chains.
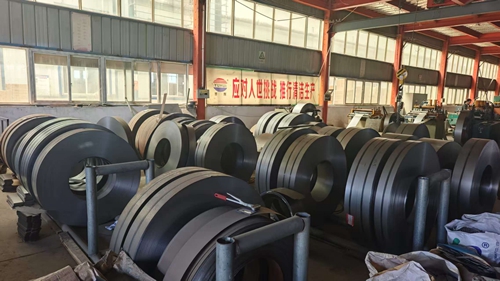
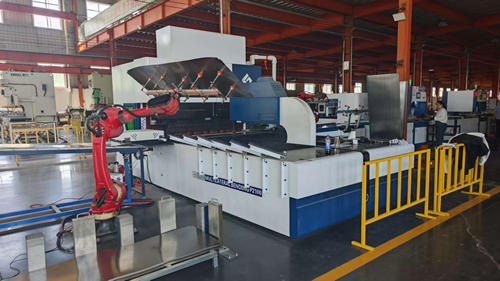
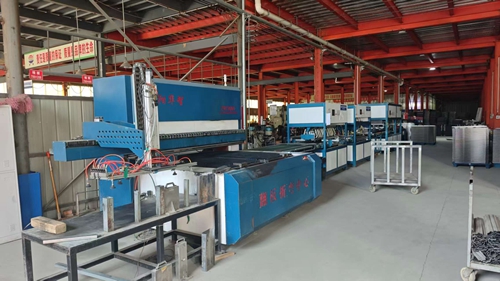
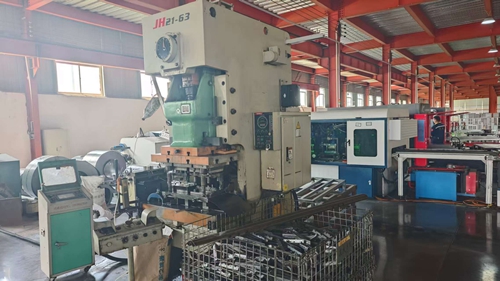
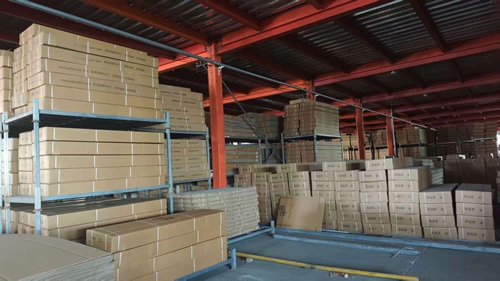
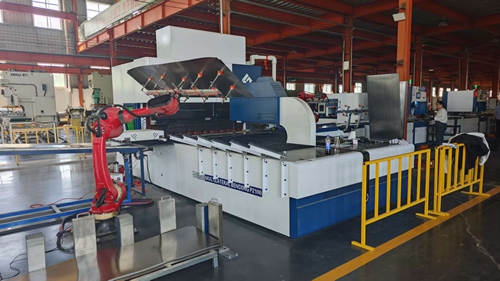
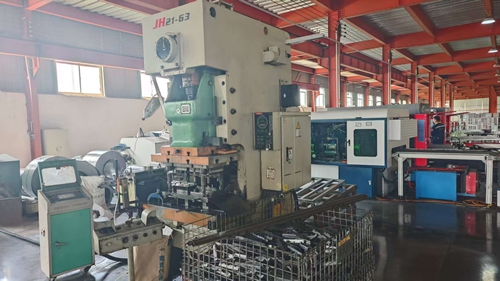
A step-by-step visual overview of automated cold-roll forming, robotic welding, and powder coating processes.
Navigating global regulatory frameworks, anti-seismic calculations, and local market engineering integration.
When procuring racking equipment internationally, engineering compliance with destination country building codes is paramount to mitigate structural liability and pass municipal safety inspections. Shenzhen Yuanzhang Trading Co., Ltd. designs systems aligned with global safety protocols including FEM 10.2.02 (European Federation of Materials Handling), ANSI/RMI MH16.1 (Specification for the Design, Testing and Utilization of Industrial Steel Storage Racks), and EN 15512 standards.
Custom structural calculations account for key local factors including:
Looking toward the future of global supply chains, industrial racking is evolving from passive steel structures to intelligent, data-connected assets. Shenzhen Yuanzhang Trading Co., Ltd. is currently researching and implementing several next-generation initiatives:
Integrating micro-load cells and IoT telemetry into main load beams to provide real-time overload alerts and continuous strain monitoring directly to Warehouse Management Systems (WMS).
Re-engineering upright column profiles and bottom guidance rails to seamlessly accommodate autonomous mobile robots and automated forklift guidance systems.
Transitioning manufacturing processes to low-temperature curing powder formulations and 100% water-recycling pre-treatment washing loops for enhanced environmental sustainability.
Comprehensive answers to crucial procurement, technical compliance, and international shipping queries.
Browse additional custom, long-span, double-sided, and specialized industrial storage solutions.
 Yuanzhang Rack