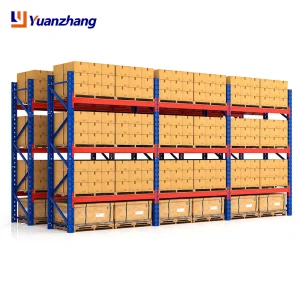
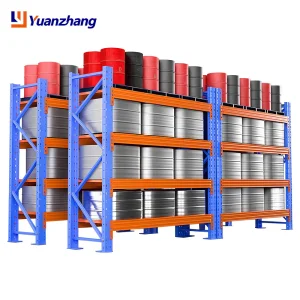
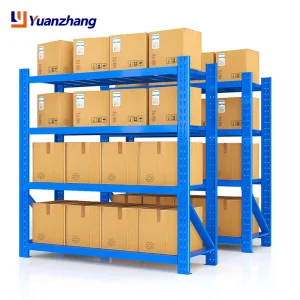
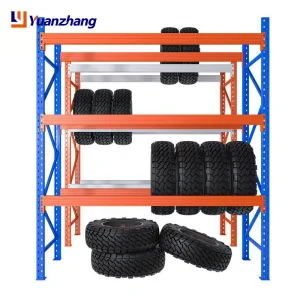
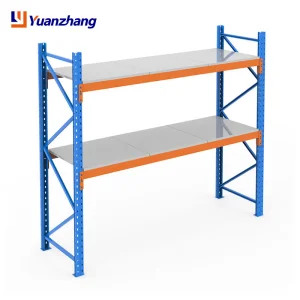
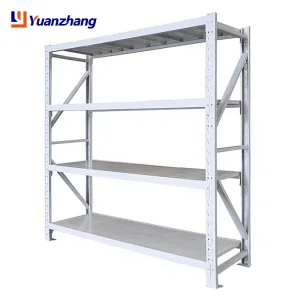
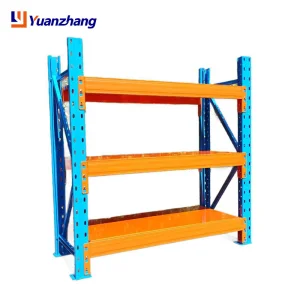
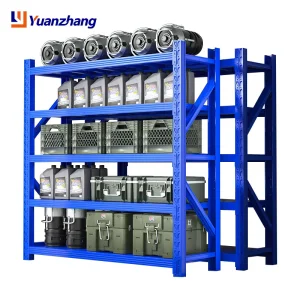
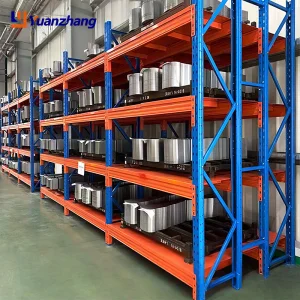
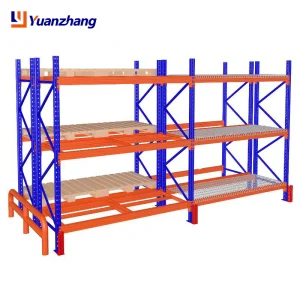
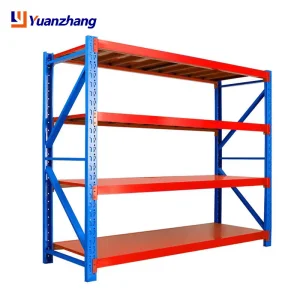
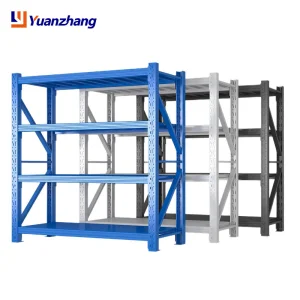
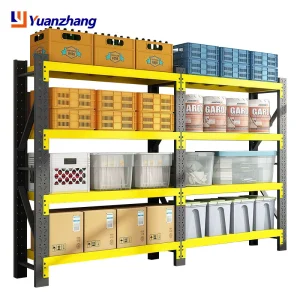
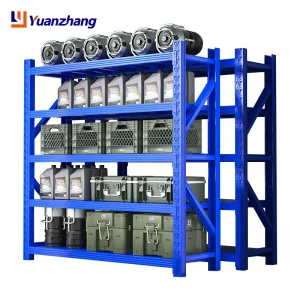
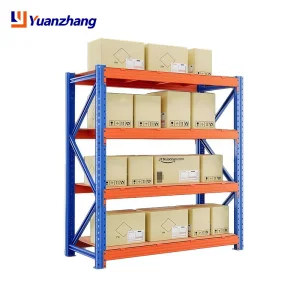
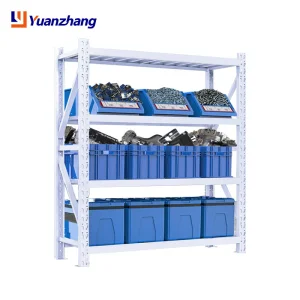
Engineered for maximum payload capacities, corrosion resistance, and optimal warehouse spatial efficiency.
Unmatched manufacturing ecosystem, economies of scale, and stringent export-grade standards.
China's integrated industrial clusters provide seamless access to superior raw materials, advanced rolling mills, and automated stamping lines, reducing production latency and ensuring uniform quality across mass-produced batches.
Leading suppliers leverage automatic roller pressing lines, robotic welding arms, and electro-static powder coating systems to deliver high-precision structural integrity and superior surface anti-corrosion performance.
Strategic locations near major international shipping ports enable streamlined export operations, robust container loading efficiencies, and reliable delivery schedules for global 3PL operators and commercial developers.
Adapting to modern supply chain demands through modular design, IoT integration, and eco-friendly manufacturing.
With warehouse real estate costs peaking globally, modern operations demand multi-tier mezzanine systems and heavy-duty pallet racking designed to maximize vertical cubic capacity without compromising structural safety.
Global B2B buyers increasingly require tailored dimensional specifications, specialized load-bearing thresholds (300kg to 500kg+ per layer), and rapid prototyping backed by dedicated engineering R&D teams.
Adherence to international eco-standards via closed-loop powder coating processes and recyclable cold-rolled steel materials ensures corporate buyers meet environmental compliance and ESG targets.
Established in 2015, Shenzhen Yuanzhang Trading Co., Ltd. is a leading manufacturer and exporter specializing in heavy-duty warehouse racking and customized industrial storage systems. Operating out of a state-of-the-art 35,000 m² production facility, we bring 12 years of deep industry expertise and 8 years of dedicated international trade experience to global logistics and commercial storage projects.
Driven by technical excellence, our operations are backed by a robust research and development center staffed with 25 expert R&D engineers. Demonstrating our strong commitment to innovation, we launched over 150 new storage solutions last year alone. We offer fully versatile OEM/ODM custom options, including specialized dimensions, weight capacity adjustments, surface coatings, and modular structural designs to meet diverse client requirements.
Quality and reliability form the foundation of our business. We enforce strict multi-stage quality control—utilizing advanced automated ultrasonic testing, raw material stress analysis, and load-bearing fatigue assessments executed by a dedicated team of 45 QA/QC inspectors.
With annual export revenue reaching $28 million USD and a resilient global supply chain network of over 800 strategic raw material and component partners, we maintain steady delivery timelines worldwide. Our primary export markets span North America, Western Europe, Southeast Asia, and the Middle East. We proudly serve a diverse spectrum of global clients, ranging from large-scale third-party logistics (3PL) providers and industrial distributors to commercial warehouse developers and retail chain enterprises.
Precision engineering from raw steel to finished industrial storage systems.
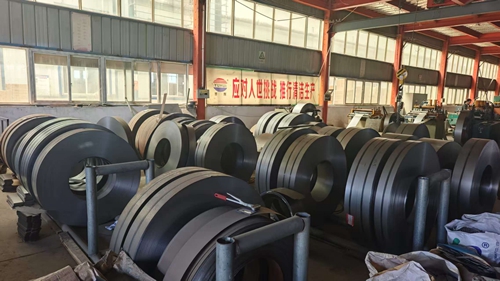
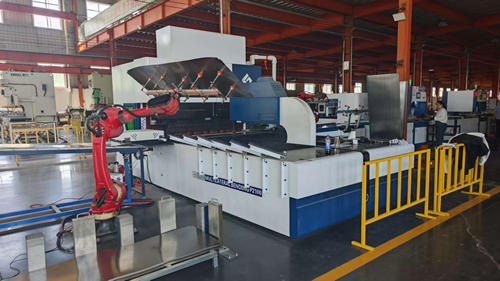
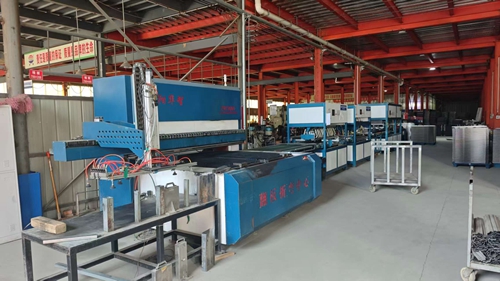
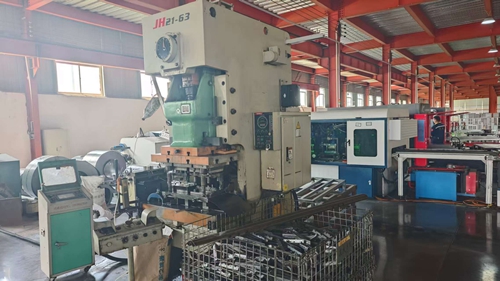
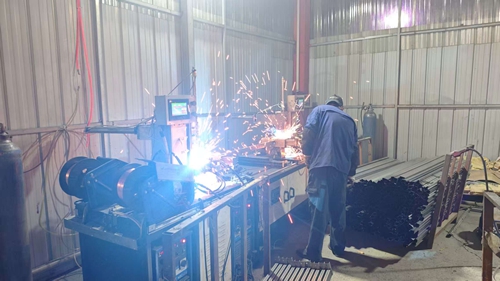
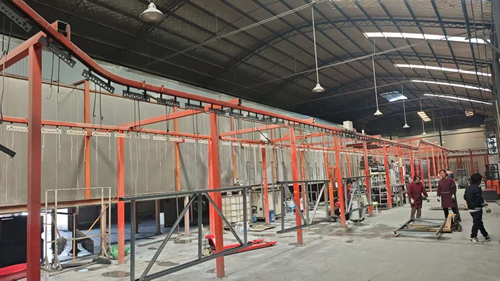
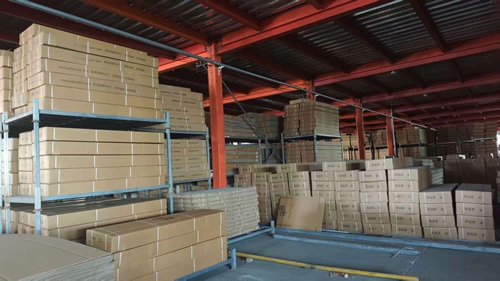
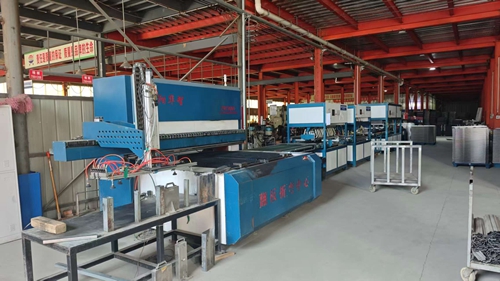
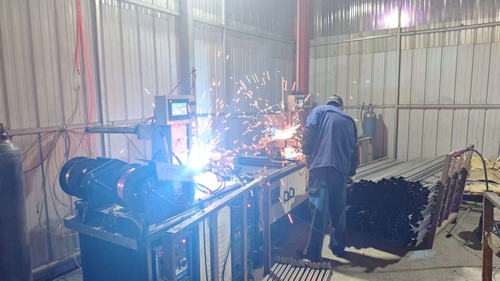
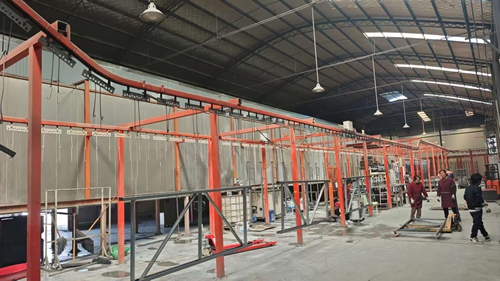
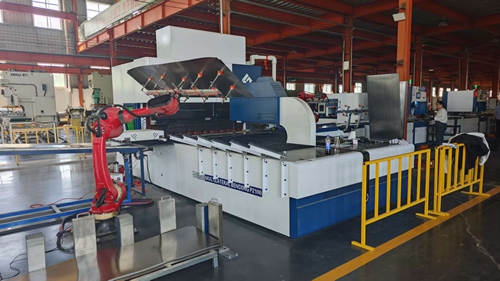
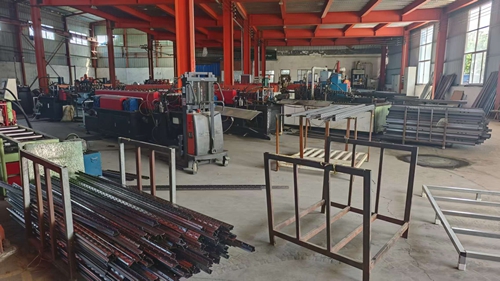
Diverse configurations designed for specialized workshop, cold storage, and multi-tier mezzanine applications.
Expert insights addressing core procurement, customization, and technical compliance queries.
Our heavy-duty storage racks are engineered to support anywhere from 100kg to over 500kg per layer, utilizing high-grade cold-rolled steel and reinforced steel beams to guarantee maximum safety and structural stability.
Yes. With 25 expert R&D engineers and advanced manufacturing machinery, we provide full OEM/ODM capabilities, tailoring dimensions, layer counts, load thresholds, and anti-corrosion powder coatings to exact client specs.
Our 45 dedicated QA/QC inspectors enforce a rigorous multi-stage quality protocol, including automated ultrasonic testing, raw material stress analysis, and rigorous load-bearing fatigue assessments.
We regularly export to North America, Western Europe, Southeast Asia, and the Middle East. Supported by a robust supply chain of over 800 partners, we maintain highly dependable shipping and delivery schedules worldwide.
 Yuanzhang Rack